


How to Select the Right Fire Protection Valve for a Sprinkler System
octubre 12, 2026
Early on a damp Thursday morning, our casting furnace operator pulls back the safety screen as white-hot molten iron pours into the ladle. A few yards away, a quality control engineer pulls a freshly cooled Válvula de compuerta OS&Y body off the production line for ultrasonic wall thickness testing. This is a typical morning inside our manufacturing workshop. We know that once these red fire valves leave our loading docks and enter ceiling networks across the world, there is zero room for failure. When a fire alarm triggers, our valves must open smoothly and deliver full water flow without hesitation.For fire protection importers, MEP engineers, and safety contractors, sourcing certified fire valves goes far beyond buying hardware off a shelf. Therefore, knowing how to select the right fire protection valve for a sprinkler system protects your building infrastructure, guarantees immediate code compliance, and ensures long-term operational peace of mind.
Global Fire Infrastructure Demand: Rapid Expansion and Strong Prospects
The global market for fire suppression hardware, fluid control valves, and structural pipe supports is expanding rapidly. Urbanization, logistics warehouse expansion, and strict municipal building code enforcement across South America, Australia, Europe, and the Middle East continue to drive high-volume demand for certified, long-lasting piping accessories.
Market analytics indicate that the global fire protection piping and fluid control sector will surpass $16 billion by 2030, maintaining a steady compound annual growth rate (CAGR) of over 6.0%.

Several key macroeconomic trends fuel this global market growth:
Strict Code Enforcement on Imported Hardware: Municipal building inspectors strictly demand verified UL-Listed, FM-Approved, and CE-marked components before issuing building occupancy permits.
Transition to One-Stop Container Consolidation: Overseas buyers are moving away from multi-vendor sourcing. Buying valves, grooved fittings, and hangers from a single manufacturer reduces sea freight expenses and customs paperwork.
Demand for Enhanced Corrosion Protection: High-humidity coastal projects and industrial plants require heavy-duty Fusion-Bonded Epoxy (FBE) and hot-dip galvanized finishes to prevent premature corrosion and line failure.
Partnering with an integrated Chinese foundry allows international procurement directors to secure stable factory-direct pricing, guaranteed certification compliance, and flexible production schedules.
How to Select the Right Fire Protection Valve for a Sprinkler System
Fire sprinkler networks rely on different valve types to manage pressure, isolate main water lines, and prevent backflow. Selecting the right valve depends directly on the installation location and functional requirements of the line.
1. OS&Y and NRS Resilient Seated Gate Valves for Isolation
Outside Screw and Yoke (OS&Y) gate valves feature an exposed threaded stem that rises as the valve opens.
Primary Function: OS&Y gate valves serve as main shutoff valves for pump houses and riser manifolds. The rising stem gives inspectors a instant visual confirmation of the open or closed status.
Underground Applications: Non-Rising Stem (NRS) gate valves keep their threads enclosed inside the valve body. Therefore, they are ideal for underground water mains or tight spaces where vertical stem clearance is limited.

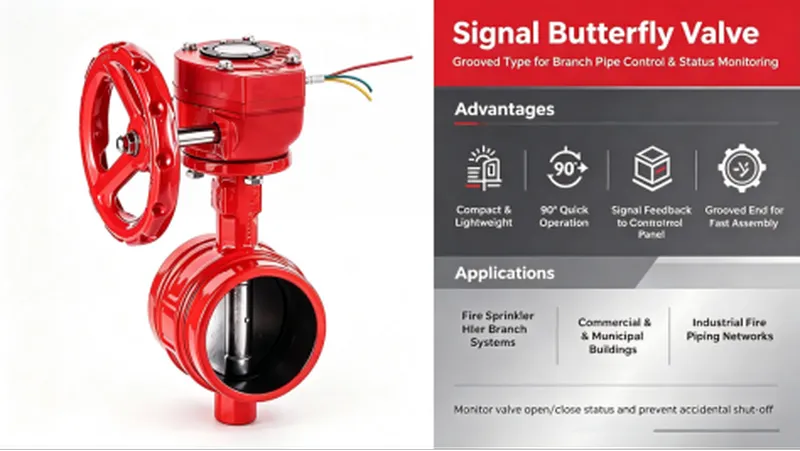
2. Signal Butterfly Valves for Branch Line Control and Monitoring
Grooved and flanged signal butterfly valves utilize a rotating disc to control water flow in fire sprinkler loops.
Primary Function: Signal butterfly valves feature built-in supervisory tamper switches. As a result, they wire directly into central fire alarm panels to alert building managers if anyone tampers with the valve position.
Key Advantages: They offer a compact footprint and lighter weight compared to heavy gate valves, making them popular for high-rise branch piping.
Fire Protection Valve Selection & Engineering Specification Matrix
| Tipo de válvula | Primary Material & Coating | UL / FM Rated Pressure | Core Application & Target Feature |
| Válvula de compuerta OS&Y | Ductile Iron Body + Red FBE Finish | 250 PSI / 300 PSI | Fire pump risers & main distribution manifolds; clear visual stem position |
| Válvula de compuerta NRS | Ductile Iron Body + Stainless Steel Stem | 250 PSI / 300 PSI | Underground supply mains & compact mechanical rooms with low vertical clearance |
| Signal Butterfly Valve | Ductile Iron Body + EPDM Coated Disc | 300 PSI | Sprinkler branch lines; built-in tamper switch integrates with fire alarm panels |
| Válvula antirretorno de vaivén | Ductile Iron Body + Stainless Hinge Pin | 250 PSI / 300 PSI | Fire pump discharge lines; automatically prevents damaging backflow & water hammer |
Fluid Tech Group: Your Trusted Global Fire Protection Partner
Delivering safe, compliant fire protection hardware requires a direct manufacturing partner with deep foundry expertise, advanced coating equipment, and seamless global export logistics.
Fluid Tech Piping Systems Co.,Ltd (known globally as Fluid Tech Group) is a premier valve manufacturer China and a reliable industrial valve supplier. Through our international portal, fireprotectionaccessories.com, operating as a specialized gate valve factory y forged steel valve supplier, we engineer, cast, machine, coat, and export a comprehensive range of UL/FM-certified OS&Y gate valves, NRS gate valves, signal butterfly valves, check valves, grooved fittings, pipe hangers, and flexible sprinkler hose drops to overseas buyers across South America, Europe, Australia, and the Middle East.
Why global safety distributors partner with Fluid Tech Group:
Direct Foundry Advantage: As an established valve manufacturer China, we operate full-scale raw casting furnaces, automated CNC lines, and electrostatic powder coating plants under one roof. Thus, we guarantee consistent metallurgical quality and fast production turnarounds.
Full Certification Compliance: Our products carry verified UL, FM, CE, and ISO credentials. Consequently, they ensure fast site inspector approval across global markets.
Heavy-Duty Corrosion Protection: We apply non-toxic, electrostatic Fusion-Bonded Epoxy (FBE) resin across our valve bodies to resist harsh soil acidity and continuous water contact.
Consolidated Shipping Support: Como líder industrial valve supplier, we pack valves, grooved couplings, flexible hoses, and pipe supports into single container loads (FCL), drastically cutting ocean freight charges and import clearance paperwork.
Global demand for certified fire safety hardware is rising fast. Partner with Fluid Tech Group to build a resilient supply chain, supply top-tier fire valves, and expand your regional market share.
Contact our technical sales team today to request product catalogs, factory test reports, or customized project quotations.